Framework overview
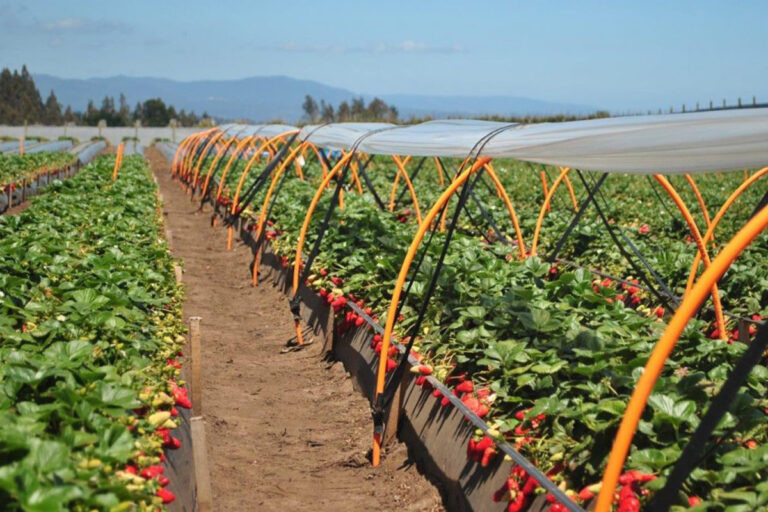
This framework lays out repeatable checkpoints, records and decision points for manufacturers of plastic film—whether the end use is packaging, horticulture, or protective covers. Start with clear acceptance criteria and layered checks that match production scale. Manufacturers who supply agricultural users already know that consistent thickness and optical performance are non-negotiable; see practical case studies for agricultural plastic sheeting that show how routine checks reduce field failures.
Core quality-control pillars
Define five pillars and make them visible at every production shift: material specification, in-line monitoring, laboratory verification, corrective action, and archival records. Each pillar maps to a short checklist so operators can close a loop quickly: measure, compare, record, act, and store evidence.
Material specification: what to require
Specify polymer type, melt index, additive load, pigment concentrations, target thickness with tolerance, optical targets (total light transmission and haze), mechanical targets (tensile and elongation), and barrier metrics if relevant. Use numeric targets instead of qualitative phrases. Attach a single-sheet spec to each incoming lot.
In-line monitoring and control points
Place fast checks where value is highest: die/film gauge, cooling roll temperature, take-up speed, and winder tension. Use non-contact thickness gauges for continuous feedback and log values at defined intervals. Log deviations that exceed a pre-set trigger and require a stop-and-evaluate decision—don’t let minor drift become a systemic trend.
Laboratory testing protocol
Reserve a small lab for confirmatory tests. Workflows should include tensile and elongation (ASTM D882), impact/puncture resistance (ASTM D1709 or applicable regional equivalent), thickness distribution with calibrated micrometers, light transmission and haze (ASTM D1003), water vapor transmission (ASTM F1249) and accelerated weathering for UV-sensitive grades (ISO 4892 or equivalent). Define sample size, sampling frequency, and acceptance bands for each test. Keep raw data and certificates for the full retention period required by customers or regulation.
Sampling strategy
Base sampling on batch size and process variability. For steady-state runs, sample at start, at steady intervals during production, and at run end. For new formulations or suppliers, increase sampling frequency. Always label samples with time, shift, roll ID, and operator. Keep physical retain samples from each production lot for the established retention period; link those samples to digital records.
Documentation structure and mandatory records
Create standardized templates: raw-material certificates, receiving inspection, in-line gauge logs, lab test reports, deviation/corrective action reports, and release forms. Use a single identifier—lot or roll number—across all documents. Store originals in a secure system and maintain an accessible summary record for customer inquiries.
Traceability and retention
Traceability must be immediate: unique lot numbers, time-stamped production logs, and supplier batch references. Adopt a clear retention policy—physical retain samples, electronic raw data, and final Certificates of Conformance kept for a defined period tied to product risk and customer needs. Make retrieval a routine drill to prove traceability works.
Supplier control and incoming inspection
Qualify suppliers with a concise scorecard: quality history, test data, on-time delivery, and change-notification practices. On receipt, verify certificate of analysis against your spec and run a quick incoming test for critical parameters. Require advance notice for formulation changes and reserve the right to audit when changes could affect performance.
Correction and escalation framework
Define three escalation levels: operator-level fixes for immediate containment, supervisor-level review for root-cause within the shift, and management-level corrective action for systemic issues. For every deviation, record the cause, corrective steps, who approved release, and verification that the fix worked. Keep closure evidence linked to the original lot record.
Common pitfalls and how to avoid them
Relying on visual inspection alone. Use numeric checks for thickness and optics. Letting in-line drift accumulate. Set triggers and stop conditions. Losing sample linkage. Use consistent naming and barcodes. Ignoring supplier notifications. Treat every supplier change as a test event. Overcomplicating documents. Keep templates short and focused on actionable fields.
Evidence, compliance and a real-world anchor
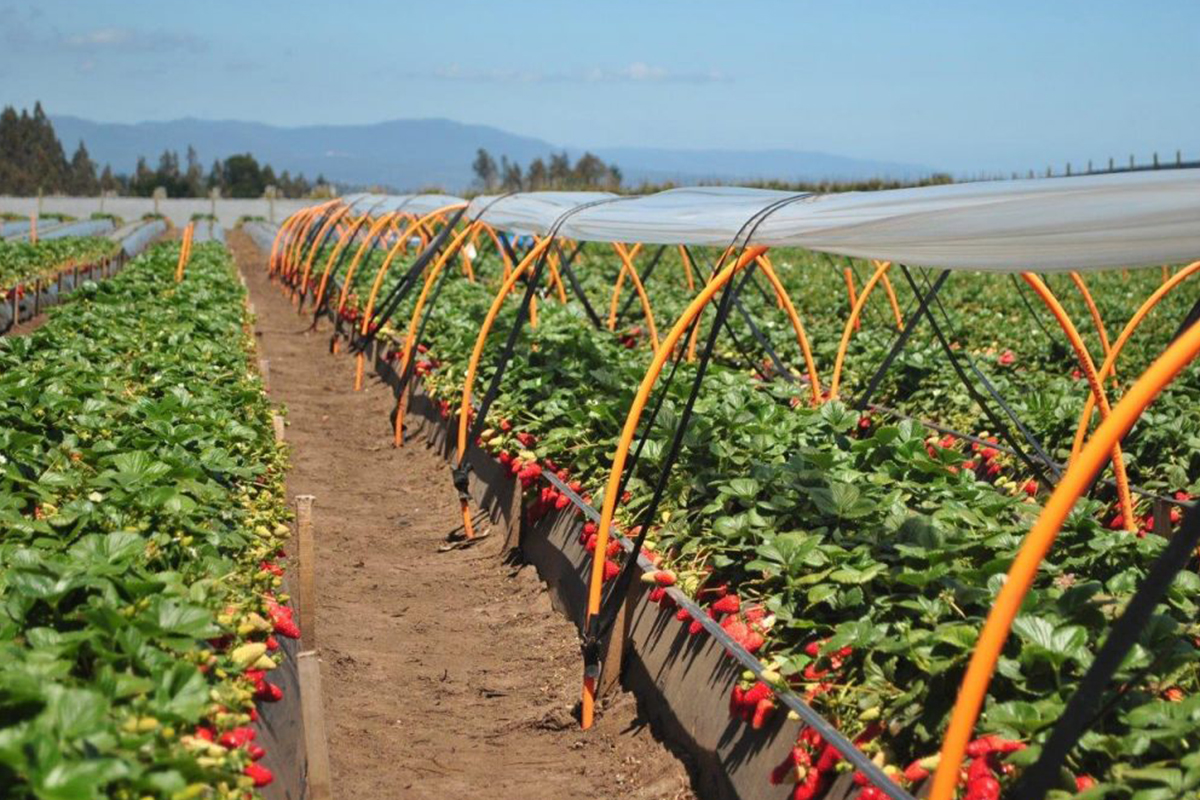
Maintain practical evidence: lab raw data, equipment calibration logs, and signed release forms. Field experience shows clarity matters—the high-output greenhouse regions near Almería, Spain, demand consistent optical performance, and growers there routinely require transmission and hail-resistance data before purchase. This industry reality aligns with documented trials and reports for clear greenhouse film, so link your lab methods to the performance metrics customers value.
Framework adoption checklist
Adopt these steps in sequence: finalize numeric specs, deploy in-line gauges, establish a small lab with core tests, implement sampling and retention rules, and train staff on escalation. Pilot the framework on one product family, measure defects and returns for a fixed period, then scale once you’ve documented improvements.
Final synthesis
Organize controls, record decisively, and keep one reliable record set that ties product to performance. That simple discipline reduces surprises, speeds decisions, and protects customers who need predictable film behavior in the field—the practical value that HGDN reflects in its product records and case work.